


Entreprise
18 November 2026
Temporary Power Distribution Boxes: Uses and Sourcing Guide
A temporary power distribution box is a portable enclosure that takes one incoming supply …
 10:15
A ligne de profilage par roulage is a sequence of stations, not a single machine. Chenlong’s equipment catalog groups them into ten types: uncoiler, leveler, straightener, servo feeder, punching machine, roll forming mill, bending machine, laser welder, cutting machine, and receiving table with palletizer. This glossary explains what each does and where the published numbers apply.
Information current as of August 2026. Every parameter below is taken from Chenlong’s published product pages and is tied to the specific line it appears on. Where a page does not disclose a value, this article says so rather than borrowing a figure from a different machine.
Read it in process order, from coil to pallet. That is how a quotation is built and how a factory floor is laid out, so it is also the order in which most specification gaps show up. Each entry gives the station’s job, what varies between configurations, and the question worth asking a supplier about it.
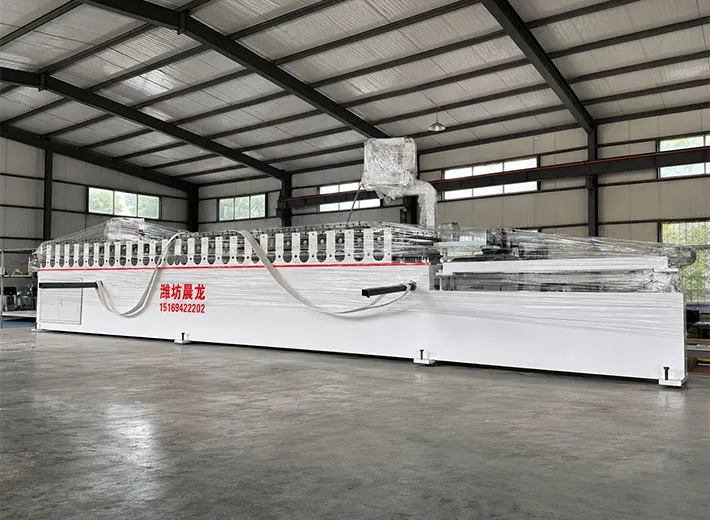
The uncoiler holds the steel coil and releases strip into the line at a controlled rate. Mechanical types rely on the pull of the downstream mill and a friction brake; hydraulic types expand and contract the mandrel under pressure and can carry heavier coils with less manual setup. Coil weight, inner diameter, and whether a coil car is included are the three variables that change the price here, and none of them are published as a fixed range — they are set per project.
À demander : pour quel poids de bobine et quels diamètres intérieur et extérieur le mandrin est-il conçu, à l’épaisseur de matériau que vous utilisez réellement ?
L’acier enroulé alimente le dévidoir et le redresseur à rouleaux. Un niveleur fait passer la bande entre des rouleaux supérieurs et inférieurs décalés afin de réduire les contraintes résiduelles avant que le matériau n’atteigne les cages de profilage. Ignorez cette étape avec une tôle galvanisée mince : la torsion apparaîtra plus tard sous la forme d’un profil fini cintré, ce qui est généralement attribué à tort à l’outillage de profilage.
Chenlong lists straightening and leveling as a separate catalog item from the leveler above. In practice the distinction is about where the correction happens: a straightening unit is often integrated as part of the feed group and handles residual camber immediately ahead of the feeder, while a standalone leveler is sized for the coil width and does the heavy stress relief. On narrow-strip lines the two are frequently combined into one frame.
The servo feeder advances a measured length of strip and stops it accurately enough for the punch to hit the same position on every part. Chenlong publishes brand options for this station: Yaskawa, Delta, or a customized alternative, listed on the cabinet line, the cable tray line, and the shelving line alike. Feeder choice is one of the few components where a buyer can specify a named supplier without redesigning the line.
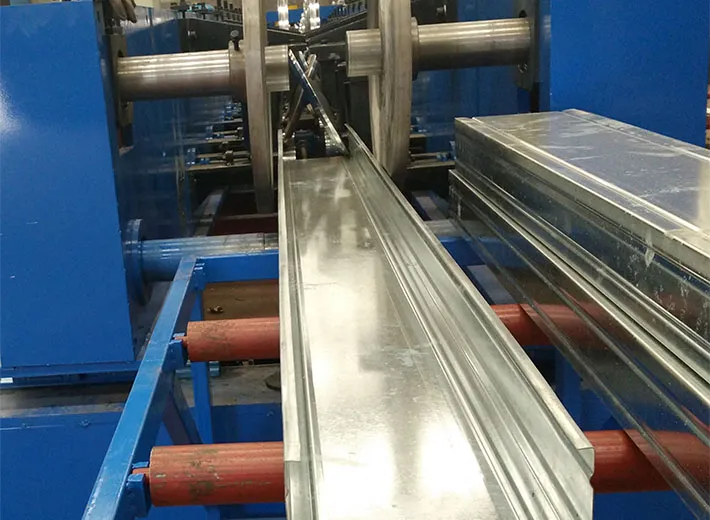
Inline punching produces the slots, keyholes, and mounting holes that make a profile usable — the perforations in a cable tray, the pitch holes on a rack upright. CNC punching changes pattern by program; hydraulic punching changes pattern by changing tooling, which is cheaper to buy and slower to switch.
Le matériau de la matrice est indiqué pour la ligne de rayonnage : Cr12MoV, SKD11 ou DC53, sélectionné selon le matériau et l’application. Ce choix détermine le nombre de frappes que la matrice peut supporter avant rectification ; il doit donc figurer dans le devis plutôt que dans une simple assurance verbale.
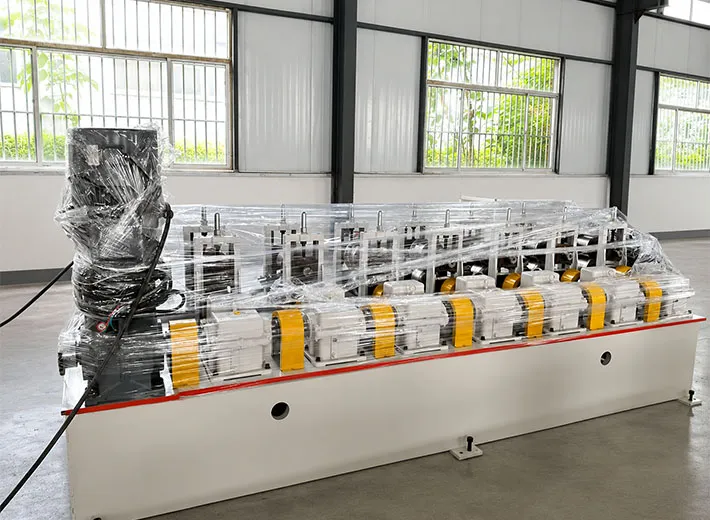
Le train de profilage est le cœur de la ligne. Une série de cages à rouleaux plie progressivement la bande plate pour lui donner sa section transversale finale, chaque cage prenant en charge une petite partie de la déformation totale. Le nombre de cages dépend de la géométrie du profil, de l’épaisseur du matériau et de la limite d’élasticité de la nuance — et non d’une catégorie de catalogue.
Chenlong describes the cable tray line as using a modular adjustable forming design intended to cover different tray specifications, which matters if a buyer expects one line to serve several product widths.
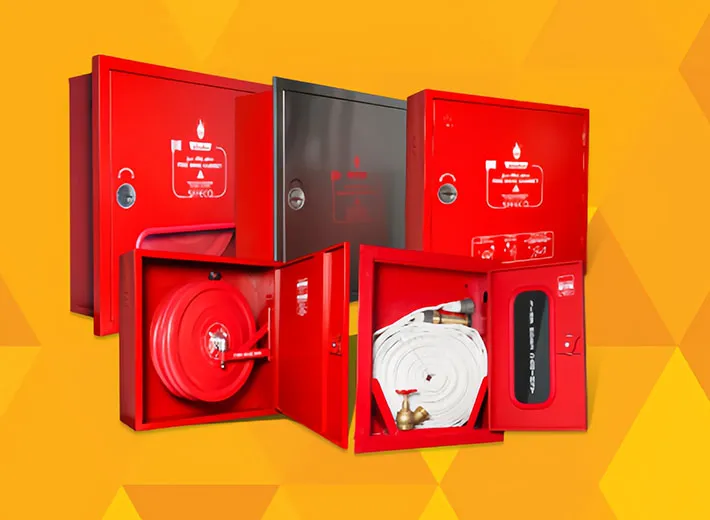
Bending handles features the mill cannot form in a continuous pass: end returns, corner folds, flanged closures on cabinet and enclosure parts. On enclosure work such as boîtiers de protection incendie casings, this station often determines whether the line ends with a finished component or a semi-finished blank that still needs a press brake elsewhere in the plant.
Laser welding joins seams and attaches reinforcement inline. It concentrates heat in a narrow zone, which limits distortion on thin gauge material compared with conventional seam methods. Whether a line needs welding at all is a product question, not an equipment question — many tray and purlin profiles ship unwelded.
Cut-to-length can happen before forming, after forming, or on the fly. Post-cut units cut the finished profile, which keeps the cross-section true; pre-cut units cut flat strip and avoid tooling wear on the blade, at the cost of tighter tolerance stacking through the mill. Cutting method is the station most often left vague in a comparison quotation, and it is one of the most expensive to change afterwards.
The output end catches formed lengths and stacks them. A plain receiving table is manual. A palletizer stacks automatically and sets the real ceiling on line throughput: a mill capable of high line speed will still run at the pace of the operator collecting parts if the output end was scoped as an afterthought.
Trois lignes de production Chenlong publient des plages de paramètres configurables. Elles se chevauchent largement du côté de la bande et divergent là où les pages cessent de fournir des informations.
| Paramètre | Ligne pour armoires et appareillage électrique | Ligne de fabrication de chemins de câbles | Ligne pour rayonnages d’entrepôt et de supermarché |
| Suitable materials | SPCC, SPHC, SGCC, SUS, aluminium, SECC | SPCC, SPHC, SGCC, SUS, aluminium, SECC | SPCC, SPHC, SGCC, SUS, aluminium, SECC |
| Largeur de la matière première | 10–2,000 mm | 10–2,000 mm | 10–2,000 mm |
| Épaisseur de laminage | 0.2–10 mm | 0.2–10 mm | 0.2–10 mm |
| Capacité de production | 0–50 m/min | 0–50 m/min | 0–50 m/min |
| Puissance du moteur de la machine | Non divulgué | Non divulgué | 3–200 kW |
| Tension | Non divulgué | Non divulgué | 110–380 V, customized to local supply |
| Matériau de l’outillage de poinçonnage | Non divulgué | Non divulgué | Cr12MoV, SKD11, DC53 |
| Servo feeder | Yaskawa, Delta, personnalisée | Yaskawa, Delta, personnalisée | Yaskawa, Delta |
| Inline punching | Oui | Yes, with servo feeding | Oui |
All of these are described as configurable to project requirements, so treat them as the outer envelope of what the equipment family covers, not as the specification of any single delivered machine. A line built to run 1.5 mm galvanized tray at a fixed width does not have a 0.2–10 mm capability; it has whatever its stands, motor, and tooling were sized for.
Supposer que les chiffres d’une ligne s’appliquent à toutes les autres. La puissance moteur, la tension et le matériau des matrices sont indiqués pour la ligne de rayonnages, mais pas pour les lignes de chemins de câbles et d’armoires. C’est une différence dans les informations communiquées, pas une preuve que les autres lignes sont identiques. Appliquer un chiffre à plusieurs familles de produits est l’erreur la plus fréquente lorsqu’on compare des fournisseurs uniquement à partir des pages qu’ils publient.
Treating forming accuracy as a single number. Chenlong’s own published material is not uniform here: catalog-level content states CNC control can reach ±0.1 mm, while the electrical and energy section of the homepage states ±0.5 mm forming accuracy. Both figures exist, and they are not interchangeable. Accuracy depends on the profile, the material grade, the thickness, and which dimension is being measured — hole pitch, overall width, and flange angle do not hold to the same tolerance. Get the number written against the specific dimension on your drawing, from any supplier, before it means anything.
Un glossaire des composants comporte un aspect lié à la conformité, car ces postes sont livrés sous forme d’un ensemble et sont généralement évalués comme un tout. La norme ISO 12100:2010, Sécurité des machines — Principes généraux de conception — Appréciation du risque et réduction du risque, publiée par l’Organisation internationale de normalisation, définit le cadre d’identification des dangers et de réduction des risques normalement utilisé pour cette catégorie d’équipements.
For machinery placed on the EU market, the European Commission states that Directive 2006/42/EC applies before 20 January 2027, and that Regulation (EU) 2023/1230 replaces that framework from that date. A line ordered now with a 40–60 business day build for custom equipment can straddle that boundary, so which framework the documentation is prepared under is a question for the order stage, not for delivery.
Acheter les postes sous la forme d’une ligne intégrée permet de bénéficier d’une architecture de commande unique, d’un seul processus de mise en service et d’un interlocuteur responsable lorsqu’une pièce profilée est hors tolérance. Contrairement aux références techniques de type manuel qui dominent les résultats de recherche sur ce sujet, la description des composants par un fournisseur indique ce qui est réellement compris dans le devis plutôt que ce qui est théoriquement possible. Mais elle est aussi rédigée par la partie qui vend la ligne ; c’est pourquoi le tableau des paramètres ci-dessus signale les données non communiquées au lieu de les inventer.
The real cost of integration is flexibility. A line engineered around one profile family runs that family well and adapts to a genuinely different cross-section only through new tooling and, sometimes, new stands. Plants with unpredictable product mixes sometimes do better with standalone machines and manual transfer between them, accepting lower throughput for the ability to reconfigure. Plants running a stable catalog rarely regret integration.
There is no published price list, and any figure quoted without your drawings is not a price. Chenlong engineers des solutions adaptées aux dessins de profilés des clients, aux spécifications des matériaux, aux dimensions des produits, à la vitesse de production requise, aux exigences de poinçonnage, au niveau d’automatisation et à la configuration de la ligne ; les prix sont donc établis projet par projet, sur devis.
The commercial terms that are published:
A: No. George T. Halmos’s Roll Forming Handbook (CRC/Taylor & Francis) is an engineering reference covering forming theory, flower design, and tooling calculation. This page is a supplier-side glossary of the machines in a production line. If you are designing roll tooling, the book is the correct source; if you are specifying or buying a line, a station list of this kind is more directly useful.
R : Cela dépend de la section transversale, de l’épaisseur et de la nuance du matériau, plutôt que d’un nombre standard ; ce nombre est donc déterminé lors de la phase d’ingénierie une fois le dessin fourni. Tout nombre de cages proposé avant l’examen d’un dessin n’est qu’une estimation.
R : Parfois. Chenlong décrit une conception de formage modulaire réglable sur la ligne de chemins de câbles, destinée à prendre en charge différentes spécifications de chemins de câbles. La portée de cette flexibilité dépend de la similarité des sections transversales : les changements de largeur et de profondeur sont plus faciles à intégrer qu’une séquence de pliage différente.
R : Le poinçonnage en ligne supprime une étape de manutention et permet de référencer la position des trous par rapport au processus de formage. Le poinçonnage hors ligne simplifie la ligne et se justifie plus facilement lorsque les motifs de trous changent constamment d’un petit lot à l’autre.
A: Positioning repeatability at the punch, and the spare parts and service network behind it. Yaskawa, Delta, and customized options are published for the cabinet, cable tray, and shelving lines, so a preferred brand can usually be specified at order stage.
A: Post-cut protects the finished cross-section and suits precise lengths; pre-cut reduces blade wear and suits high-volume identical parts. State your length tolerance in the enquiry and let it decide, rather than accepting whichever method the quotation defaults to.
Chenlong Technical Team — Corporate Technical Author, Weifang Chenlong Intelligent Technology Co., Ltd.
Le Chenlong Technical Team represents the company’s engineering and R&D expertise in cold roll forming equipment, customized automated production lines, tooling, and precision cold-formed steel profiles. Chenlong has been engaged in cold roll forming manufacturing since 2006 and operates in-house manufacturing facilities supported by CNC machining, tooling capabilities, custom engineering, and a professional R&D team. Its technical work covers applications in warehousing and racking, electrical and energy equipment, fire protection, construction, automotive manufacturing, and customized industrial profile production, serving customers in more than 50 countries.
A temporary power distribution box is a portable enclosure that takes one incoming supply …
Seven electrical panel board types explained for cabinet and switchgear manufacturers, plu…
Nous vous répondrons dans les 24 heures. En cas d'urgence, veuillez ajouter WhatsApp/WeChat : +8613863639320,. Ou appelez directement +8613863639320.
*Nous respectons votre confidentialité et toutes les informations sont protégées.
Nous n'utiliserons vos informations que pour répondre à votre demande et n'enverrons jamais de messages électroniques ou promotionnels non sollicités.